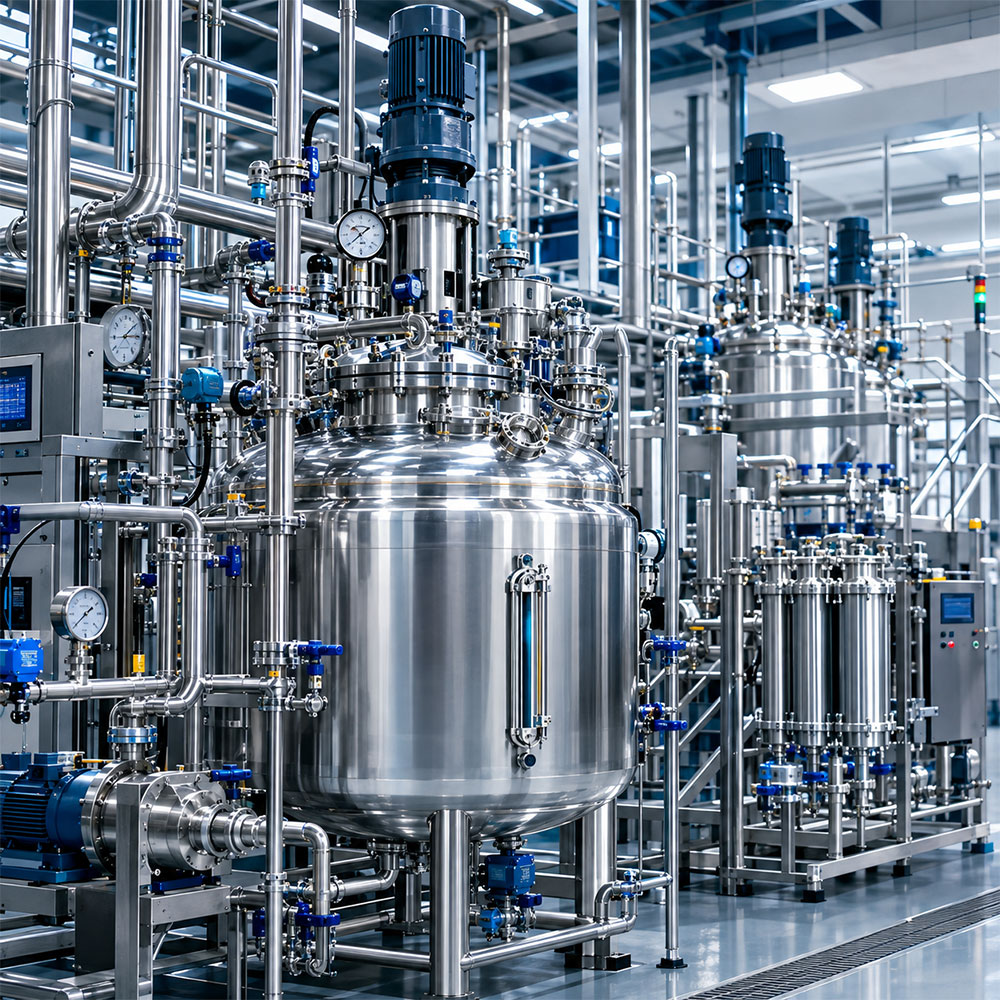
Advanced Chemical Processing Infrastructure
Purpose-built manufacturing systems designed for controlled processing, consistent quality and scalable production.
// ABOUT PHARMFIELD LABORATORIES
Pharmfield Laboratories is engaged in the manufacturing and supply of pharmaceutical intermediates and specialty chemical products, supporting the evolving needs of pharmaceutical manufacturers with consistent and dependable solutions.
From process development to scalable production, our focus remains on precision, consistency, and operational excellence. We work closely with our customers to deliver dependable products and build lasting partnerships based on quality, technical capability, and trust.
// OUR PRODUCTS
Specialized chemical intermediates manufactured for dependable performance, scalable production, and pharmaceutical API synthesis.
Essential chemical building blocks supporting pharmaceutical intermediate and API manufacturing requirements.
Specialized chemical products supporting pharmaceutical manufacturing and diverse chemical processing requirements.
// RESEARCH & DEVELOPMENT
Our R&D approach combines process knowledge, analytical expertise, and continuous improvement to develop efficient, consistent, and scalable pharmaceutical intermediates.
Developing and refining chemical processes with a focus on efficiency, consistency, quality, and commercial scalability.
Supporting the transition from laboratory and development stages to efficient and controlled commercial production.
Focused analytical evaluation and process monitoring to support product quality and manufacturing consistency.
Continuously improving processes and manufacturing practices to enhance efficiency, consistency, and reliable supply.
// WHY CHOOSE US
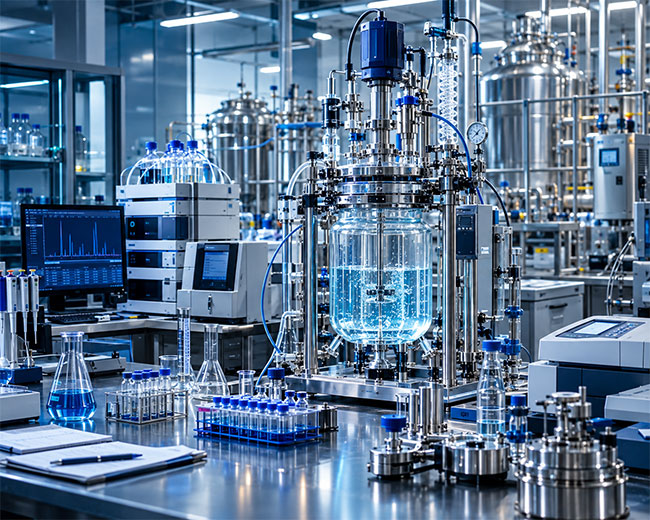
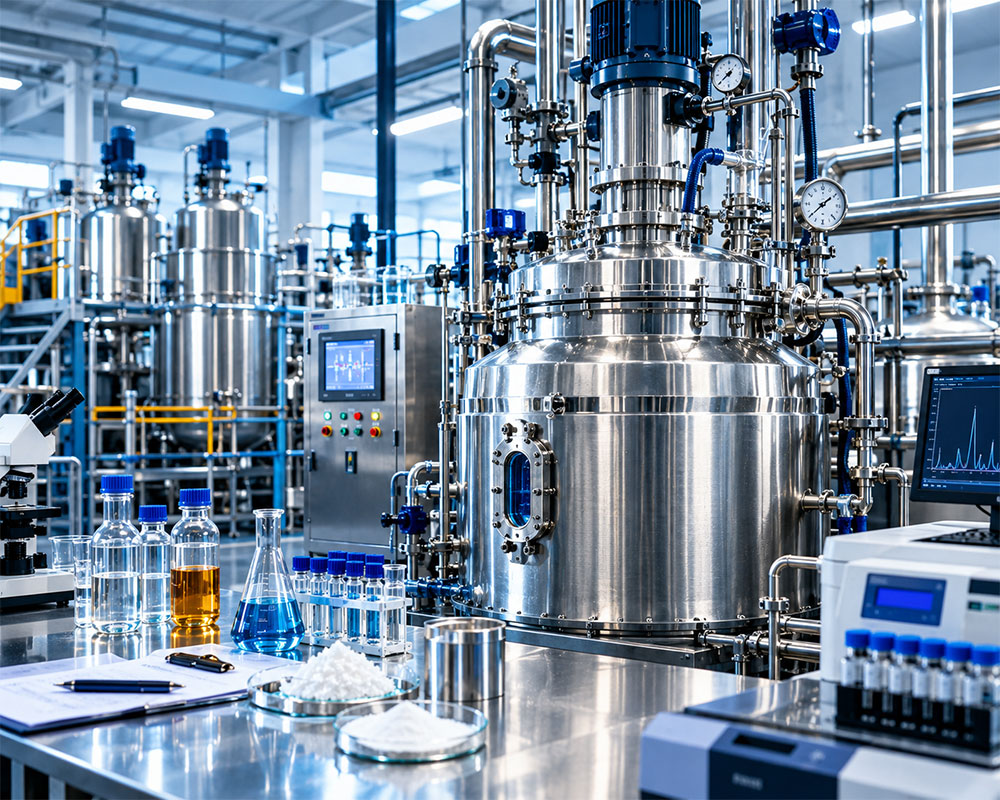
Our manufacturing infrastructure combines modern process equipment, controlled production systems and technical capabilities to support consistent pharmaceutical intermediates and specialty chemical manufacturing.
Purpose-built manufacturing systems designed for controlled processing, consistent quality and scalable production.
Modern reaction, mixing and processing systems designed for controlled and repeatable chemical manufacturing.
Dedicated technical capabilities supporting process development, optimization and scale-up activities.
Quality-focused testing and monitoring capabilities supporting product consistency throughout manufacturing.
Organized material handling and storage systems supporting safe, efficient and reliable production operations.